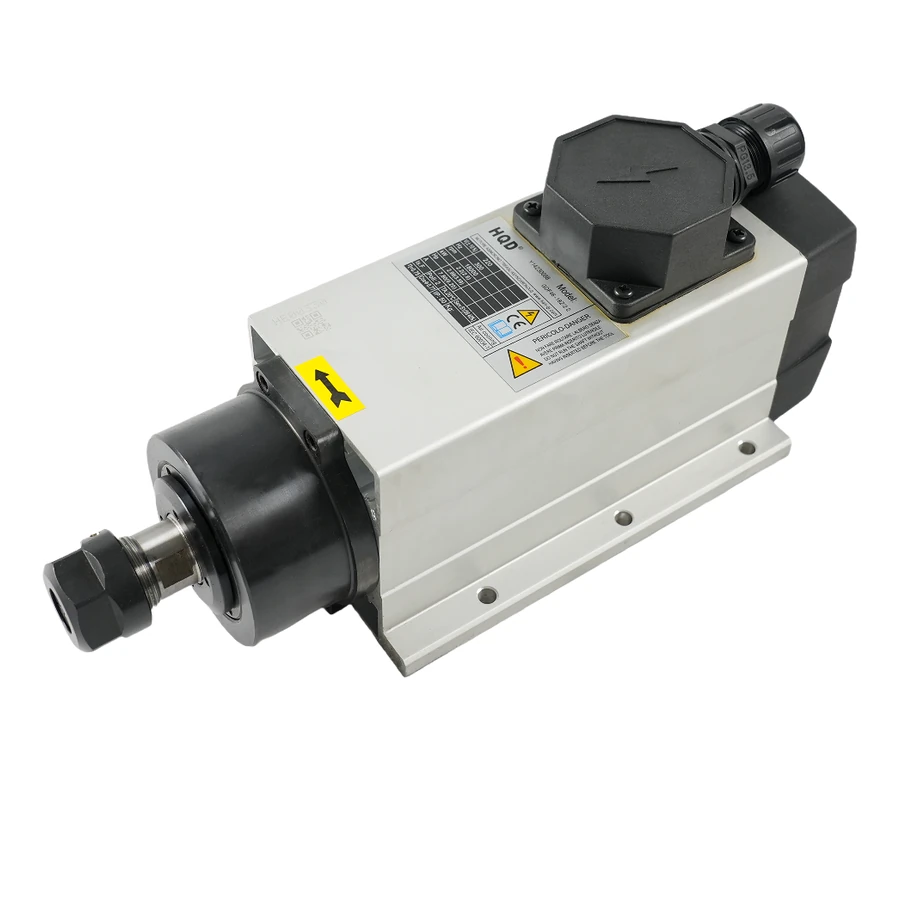
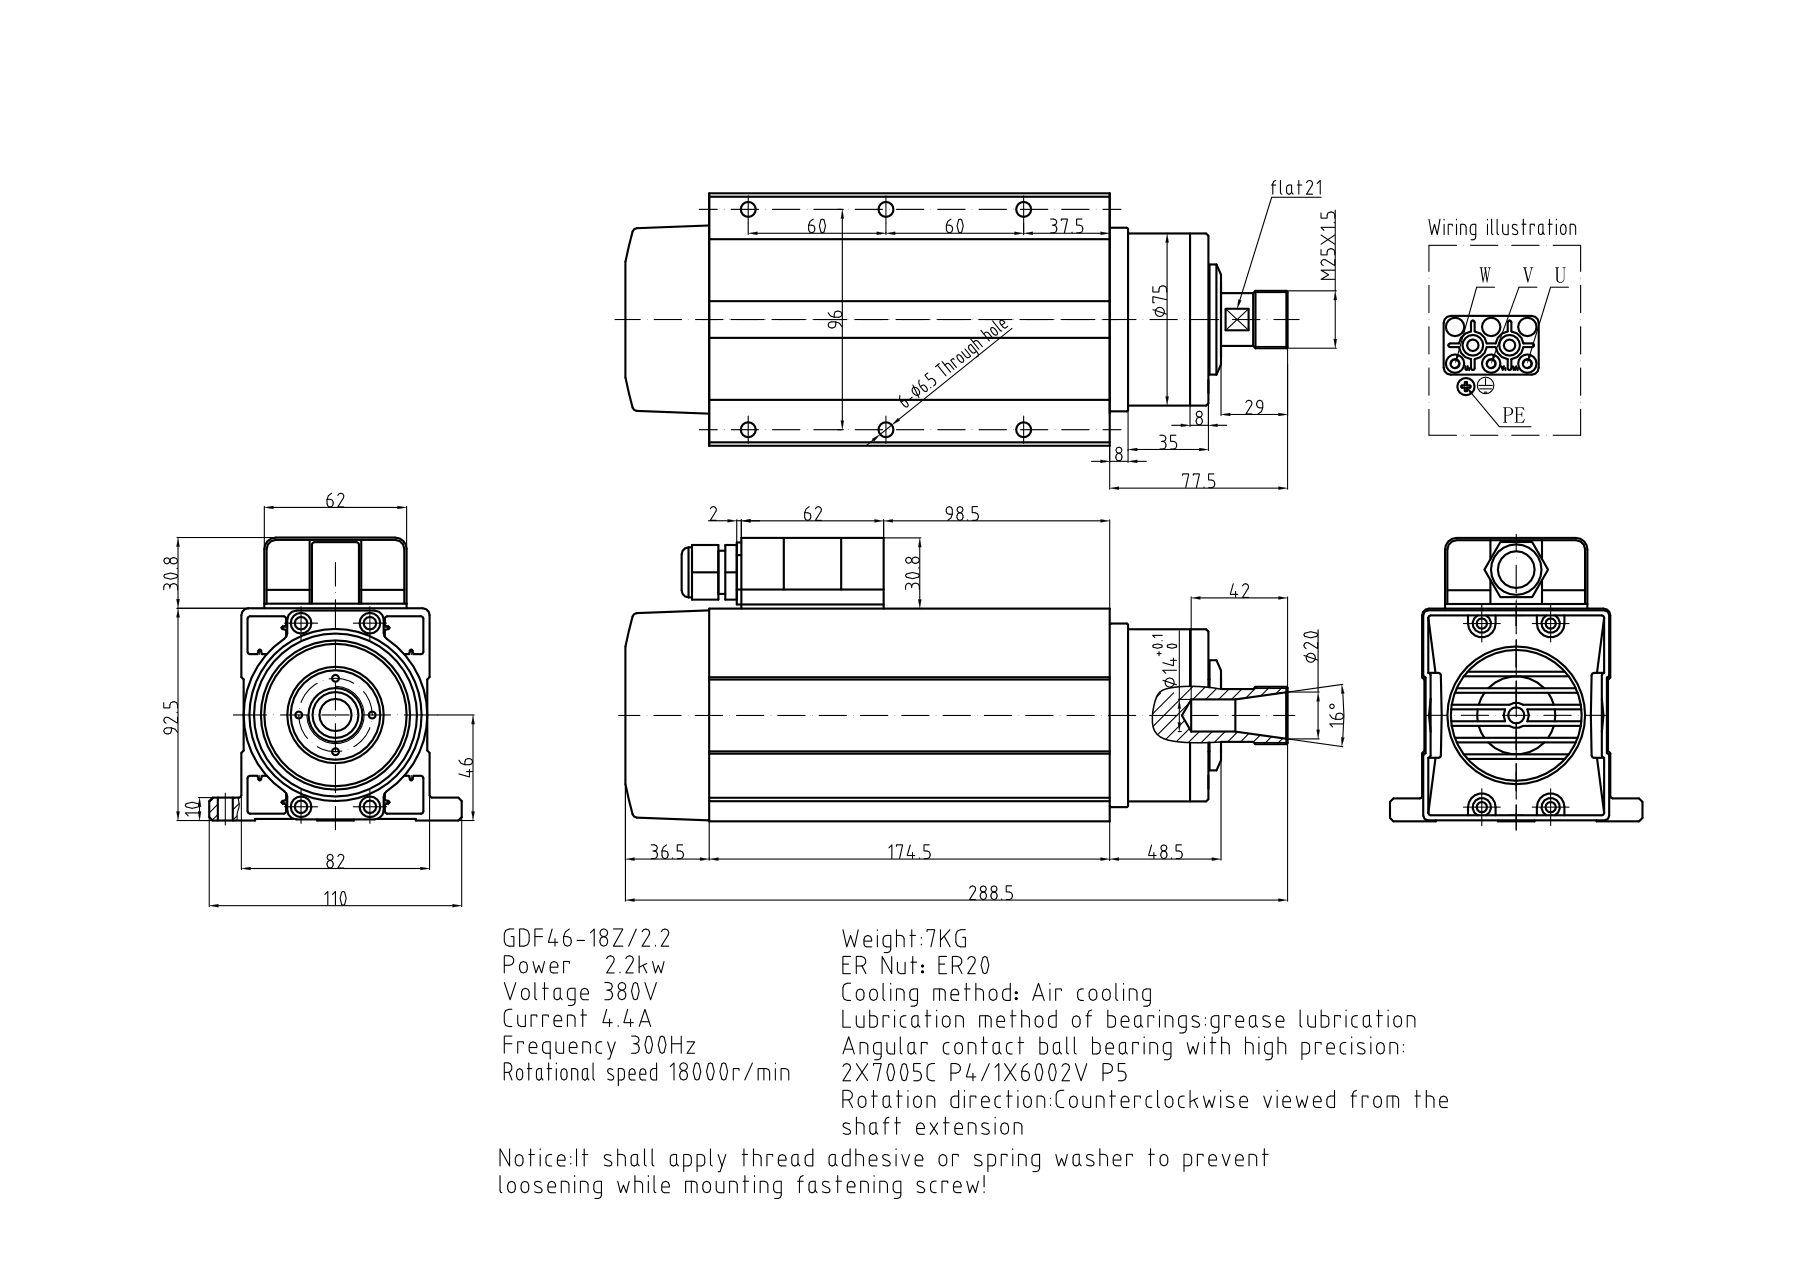
Choose from the process and fixing architecture
GDF46-18Z/2.2 Base Mount is a candidate when the process uses manual ER20 tooling and the documented 18,000 rpm point, and the machine supports the base interfaces. Begin with cutter and working speed, then assess winding, drive, fixing and airflow. A process needing a different working point or support arrangement may lead to another comparison even when 2.2 kW looks suitable.
For engraving or milling, provide material, cutter geometry, shank diameter, projection, load cycle and machine stiffness. These conditions support a suitability discussion. The motor and outline figures alone do not establish feed rate or surface finish. Include the fixture and enclosure if the assembly must fit an existing machine, so the selection considers the actual support and cooling path.