Key Requirements and Configuration Checks
- Keep the building supply, drive input and motor winding separate.
- Compare output current and frequency alongside voltage and power.
- Treat range curves, duty and auxiliaries as distinct matching requirements.
Match the proposed configuration to its applicable drawing, operating data and machine requirements. Resolve mounting dimensions, auxiliary services and operating limits before accepting a spindle for the intended installation.
| Decision | Useful evidence |
|---|---|
| Motor | Exact winding, nameplate and original operating data |
| Drive | Input/output ratings, frequency and applicable control functions |
| Machine | Speed commands, status, protection and auxiliary-service design |
Start with the exact spindle winding
Write the complete spindle code, physical variant and selected winding before selecting a VFD. A motor offered in two voltage configurations is not specified until one configuration is chosen. Keep current with its voltage so the supplier and integrator can compare the same assembly. Nameplate and supplied-unit documents take precedence over a remembered value from another product.
GDL120-30-24Z/5.5 provides a useful example: the catalog shows 220 V/19 A and 380 V/11 A windings, both at a 24,000 rpm, 800 Hz rated point. These are alternative documented pairs. A record containing 220 V from one option and 11 A from the other would describe neither winding. Include the selected pair in the quotation and drive-matching record.
Separate three electrical descriptions: the available building supply, the drive's input rating and the drive's motor output. The installation must address each one. A building voltage does not by itself identify the motor winding, and a drive's input label is not a complete statement of its output capability. Have the electrical integrator establish the complete supply and drive arrangement.
If an existing nameplate differs from catalog information, retain the plate photograph and the exact source document rather than combining their values. Resolve the supplied motor configuration before selecting commissioning settings. Qualified electrical work and the installation design must follow the applicable spindle and drive instructions, using the accepted winding, operating data and machine requirements as their basis.
Compare the drive rating as a set of requirements
Collect the drive's full model and rating, including the manual for that exact version. Record applicable input supply, rated output current and voltage, output-frequency capability and operating conditions. Identify the available motor-control methods and any restrictions relevant to the proposed high-frequency spindle. A series-level drive name may cover several sizes or options, so keep the full code.
A nominal kW match does not establish current capacity or frequency suitability. Different windings can have different current requirements for the same spindle output. Drive ratings also carry their own operating and environmental conditions. Compare the applicable rating with the chosen motor rather than assuming that a larger advertised power class resolves every requirement.
| Matching field | Spindle evidence | Drive evidence |
|---|---|---|
| Voltage | Selected winding or documented curve | Applicable motor-output specification |
| Current | Selected nameplate/configuration value | Rated output under intended conditions |
| Frequency | Rated/maximum point or supported range | Frequency capability in the chosen control mode |
| Operating cycle | Required working point and duty evidence | Applicable rating and operating restrictions |
| Control | Machine speed/run/status requirements | Available commands, feedback and protection functions |
| Auxiliaries | Fan, sensor, release and fitted feedback details | Separate supplies or interfaces in the machine design |
Use the table to identify what is already supported and what information remains missing. A supplier's statement that a drive suits a spindle should identify the exact pair and conditions. Keep that evidence with the installation record so the decision can be reviewed when a motor or drive is replaced.
Equal RPM can require different electrical frequency
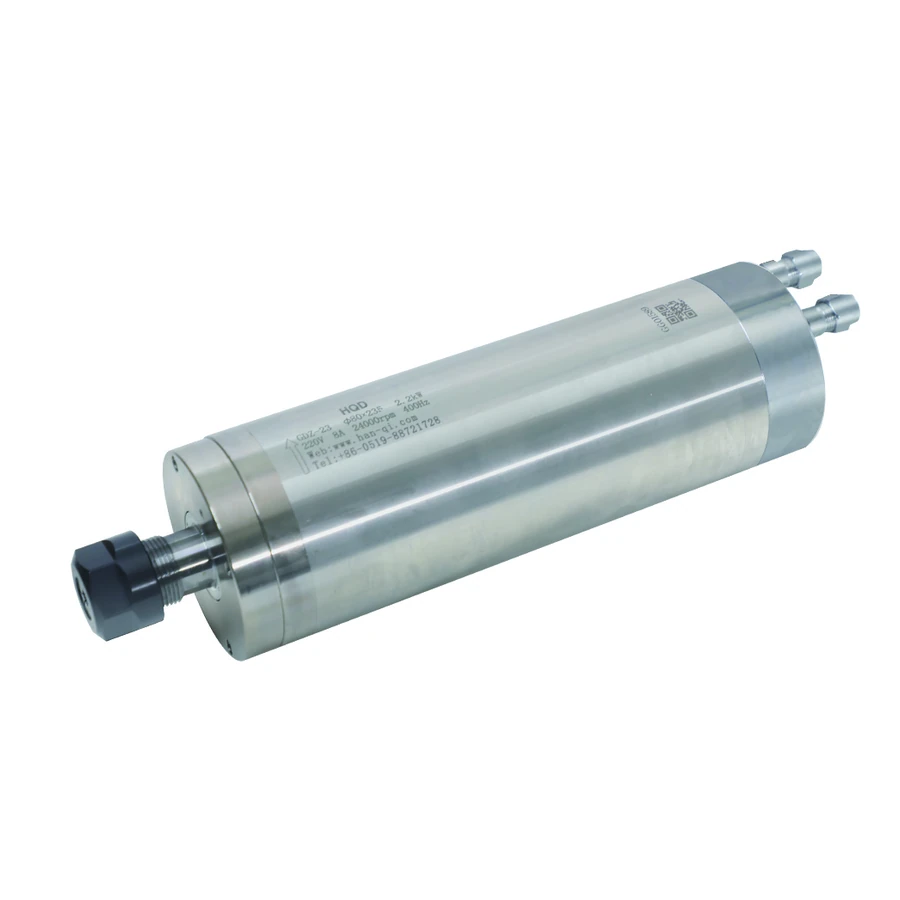
Compare frequency directly from the spindle data. GDZ-23 is rated at 24,000 rpm and 400 Hz, while GDL120 is rated at 24,000 rpm and 800 Hz. GDL80-20-24Z/2.2B also uses a 24,000 rpm, 800 Hz rated point. Equal speed therefore does not establish a shared drive limit or parameter set.
For a synchronous-speed sanity check, n = 120f/P, where n is rpm, f is frequency in Hz and P is the number of poles. Four poles at 800 Hz gives 24,000 rpm; two poles at 400 Hz gives the same calculated value. The equation helps explain the difference, but it is not a substitute for the supplied motor data or a method for assigning an undocumented pole count.
Keep rated and maximum points separate. GDL40.5 is rated at 18,000 rpm and 300 Hz, with a distinct maximum of 24,000 rpm at 400 Hz. Entering only 24,000 rpm omits that distinction. A speed command, a drive-frequency limit and the spindle's permitted operating point need a consistent interpretation in the machine design.
Review the drive manual for frequency capability in the intended control mode. A general product headline may not describe every mode or feature. Do not infer 800 Hz suitability from a low-frequency demonstration or a matching kW label. The integrator should establish how requested machine speed maps to the correct motor operating command.
Compare four HQD electrical records
These examples illustrate different matching questions rather than recommended drive models. Keep the cooling and tooling configuration with the motor identity because additional services can affect the machine integration. Use the linked product data and original drawing to complete the selected assembly.
| HQD example | Winding or curve data | Frequency and speed | Main matching issue |
|---|---|---|---|
| GDZ-23 | 220 V/8 A or 380 V/4.4 A | 400 Hz; 24,000 rpm rated | Select and retain the correct winding pair |
| GDL40.5 ISO20 | 220 V/7.8 A winding; separate 24 V DC auxiliaries | 300 Hz/18,000 rpm rated; 400 Hz/24,000 rpm maximum | Separate operating points and auxiliary functions |
| GDL120 BT30 | 220 V/19 A or 380 V/11 A | 800 Hz; 24,000 rpm rated | Review high-frequency output and chosen current |
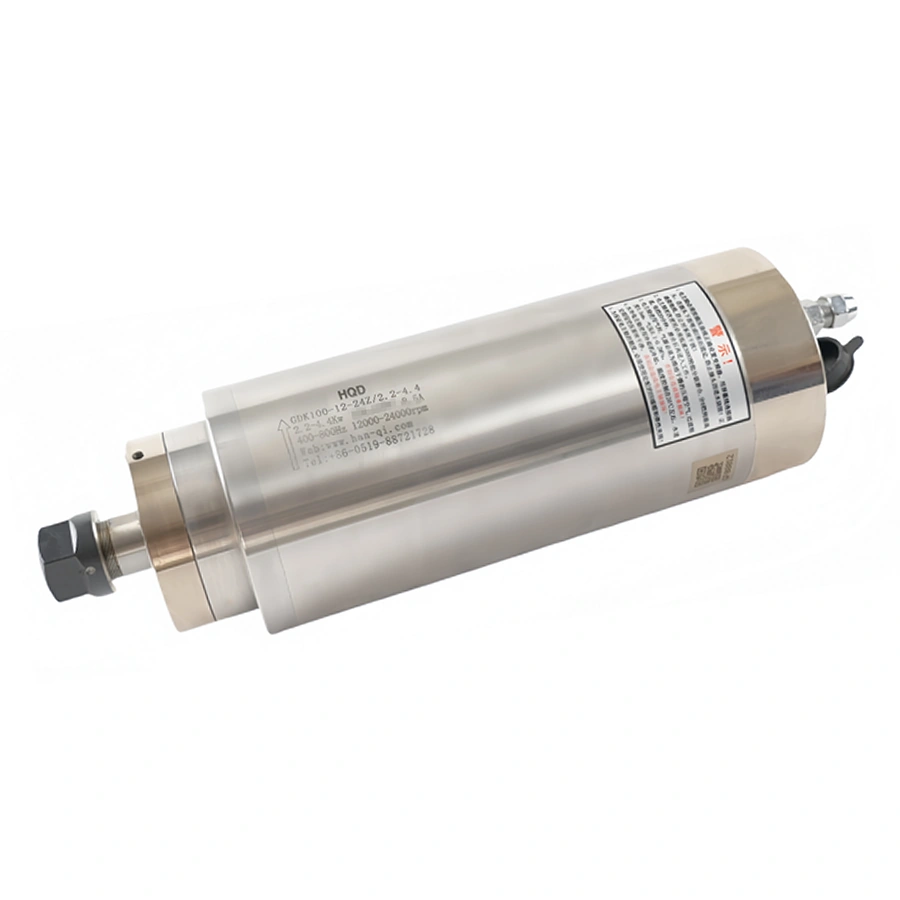
| GDK100 range model | 269–380 V operating curve; 6.8 A catalog value | 400–800 Hz; 12,000–24,000 rpm range | Read the complete curve and its conditions |
GDK100's curve endpoints should not be reformatted as two winding choices. Conversely, GDL120's two documented winding pairs should not be interpreted as one continuous voltage curve. These forms of information answer different questions, even though they both contain voltage numbers.
If the drive is already installed, compare its complete specification against the chosen row before deciding to retain it. If the spindle has not been selected, use the machine requirements to narrow the candidates first. The selection guide keeps the working point and installation discussion ahead of a generic drive purchase.
Read voltage, power and torque with the original curve
Range-model data needs the original source and its labels. GDK100-12-24Z/2.2-4.4 shows 269–380 V over 400–800 Hz, alongside separate power and torque curves. Those endpoints describe the documented operating relationship. They are not permission to order an arbitrary winding or to replace the curve with one constant voltage/frequency ratio.
The same source identifies S1/S6-20% at TA20°C conditions and a 2.2 kW rated catalog value. Preserve the conditions when comparing a higher curve output. A number in the model suffix does not establish continuous output throughout the range. The power and torque guide explains how to interpret the source and calculate torque at a documented point.
For drive review, mark the required speed on the source and record the associated evidence. If the intended operating point falls outside the documented region, request the applicable motor information before making assumptions. The drive integrator needs a supported relationship and duty, not an extrapolation from the largest number in a code.
Retain the source revision with the accepted configuration. This matters when a later purchase has a similar name but different supplied data. A short matching table is convenient for quotation, while the original curve remains necessary for technical review.
Compare the actual operating cycle and applicable ratings
Describe the intended cycle: cutting, non-cutting rotation, positioning, exchanges and any periods without rotation. Keep the required working point and the spindle's documented duty together. An installation evaluated for one production sequence should not be assumed suitable for another merely because the maximum RPM remains unchanged.
A conditioned power value and an unqualified continuous requirement are different. The GDL70 air-cooled configurations, for example, show 9 kW with S6-60% at TA20°C. That label must remain visible when evaluating the motor and supporting installation. Do not convert it into a universal 9 kW continuous requirement or assert a cutting capability from the headline value.
The drive has its own rating conditions and operating requirements. Have the integrator compare them with the selected motor, machine environment and production cycle. Changes to acceleration, control method or other operating behavior require review under the applicable equipment instructions, with the accepted settings linked to the exact spindle-drive pair and the machine functions they serve.
Record the accepted cycle and evidence rather than treating a short rotation test as proof of production suitability. The final process evaluation should use the agreed tooling and conditions, while electrical commissioning follows the supplied equipment instructions.
Understand parameter meanings before translating them into a menu
Drive manuals commonly distinguish motor nameplate data, speed or frequency limits, control method, command sources and protection behavior. These categories explain what an integrator must establish. Their names and implementation vary by drive; a parameter number from one manual should not be copied into another model's menu.
Motor voltage, current, nominal frequency and nominal speed describe the supplied motor configuration. A maximum frequency or speed limit serves a different purpose. Command scaling determines how the machine's requested speed is interpreted. Read those fields separately so a maximum point is not entered as a rated value or an input voltage as a winding voltage.
| Parameter category | Meaning to establish | Evidence needed |
|---|---|---|
| Motor identity/data | Which supplied motor the drive controls | Exact plate, winding and source data |
| Limits | Permitted operating envelope | Spindle and machine requirements |
| Control method | Applicable motor-control approach | Exact drive/manual and motor information |
| Command source/scaling | How run and speed requests are interpreted | Machine-control and drive-interface design |
| Status and protection | How the machine observes and responds | Fault, ready and required protective functions |
Map the accepted motor data, limits, command sources and protection requirements to the exact drive manual with qualified personnel. Confirm that the selected drive version and control mode support the required spindle frequency and operating conditions. A manual illustrating common motor-data and control categories does not establish suitability for another spindle-drive combination; retain the supporting model-specific evidence with the machine configuration.
Separate fan, sensors, release and feedback from motor power
Identify auxiliary functions from the exact supplied wiring drawing. GDL40.5's 24 V DC fan and sensor circuits are separate from its 220 V spindle winding. The motor VFD output is not a general auxiliary supply. Record the source, connection and control purpose for each function in the machine design.
ATC adds release and state requirements. The controller needs the appropriate information for its exchange sequence, and the machine integrator must establish the response to missing or contradictory states. Pneumatic release and tool handling are separate from speed control. The ATC integration guide outlines the whole-system review.
Feedback also needs actual hardware evidence. A connector reserved for an encoder does not show that an encoder is fitted. GDL110 is listed without an installed encoder. If a control function requires feedback, identify the fitted device and applicable signal information before planning that function.
Keep a service and function list alongside the motor record. Identify the connection supplying spindle rotation, each cooling auxiliary and every signal or control connection used for another machine state. Link their voltage, function and interface requirements to the supplied wiring documents so the installation can be reviewed without inferring circuit functions from connector appearance.
Resolve mismatches before reusing a drive
Classify each field as supported with evidence, requiring a designed change, or unresolved. A drive with adequate current but an unsuitable frequency capability is not a completed match. A correct motor-output rating with a different command interface still requires machine-control integration. Keep each consequence visible rather than averaging the results into a general compatible label.
For a hypothetical replacement from GDZ-23 to GDL80 ISO20, both motors have a 2.2 kW rated value and a 24,000 rpm rated speed, but the candidate uses an 800 Hz point and ATC tooling. The project needs frequency review plus release, sensing, holders and measurement. The electrical comparison is one part of that conversion, not the whole proposal.
Document any change to the drive, winding choice, control interface or supporting equipment. Retain the old configuration as history and the accepted new configuration as the operating record. Commissioning and process evaluation should follow the integrator's agreed plan and the applicable equipment instructions.
Retain an electrical handover record
After the exact motor and drive have been accepted, retain their full identities and the source documents used in the comparison. Keep the selected winding, working point and duty with the applicable drive rating and control-method evidence. The record should explain why the pair was selected without requiring another technician to reconstruct an informal exchange of photographs.
The qualified integrator should retain the commissioned drive configuration using the method supported by that equipment. Link it to the machine and motor identity, along with any interface or auxiliary-circuit changes. A configuration backup is useful only when its intended assembly is clear; it should not be labeled as a universal HQD setup.
Add the agreed operating checks and results, plus the representative process conditions evaluated by the machine project. Separate parameter configuration, electrical commissioning and process acceptance. Those records answer different questions when a future fault appears or a different cutter and cycle is introduced.
For maintenance or replacement, compare the proposed change with this accepted baseline. A changed winding, drive version, control function or production cycle can require another review even when the spindle code or headline power appears familiar. Update the relevant drawings and configuration record after acceptance so the next service begins with the actual installation.
Send a complete spindle-drive matching record
A useful inquiry includes the spindle code and variant, chosen winding, required working speed and duty, drive model and full input/output data. Add the available building supply, machine-control interface and auxiliary requirements. Photograph the existing plates when reviewing a replacement and attach the original range curve when it governs the operating requirement.
Name open questions precisely: missing current for a supplied winding, frequency capability in a selected mode, or an unresolved control function. The supplier can then identify the needed document rather than answer a generic question about whether two power labels match. Include which components must remain and which changes the machine builder can accept.
Keep the accepted spindle-drive comparison as a table linked to the source documents. Record the exact motor and drive, the selected winding, operating point, duty and required control functions. After the machine integration is accepted, qualified commissioning should establish the actual settings and operating baseline, with the resulting configuration retained for maintenance and future replacement review.