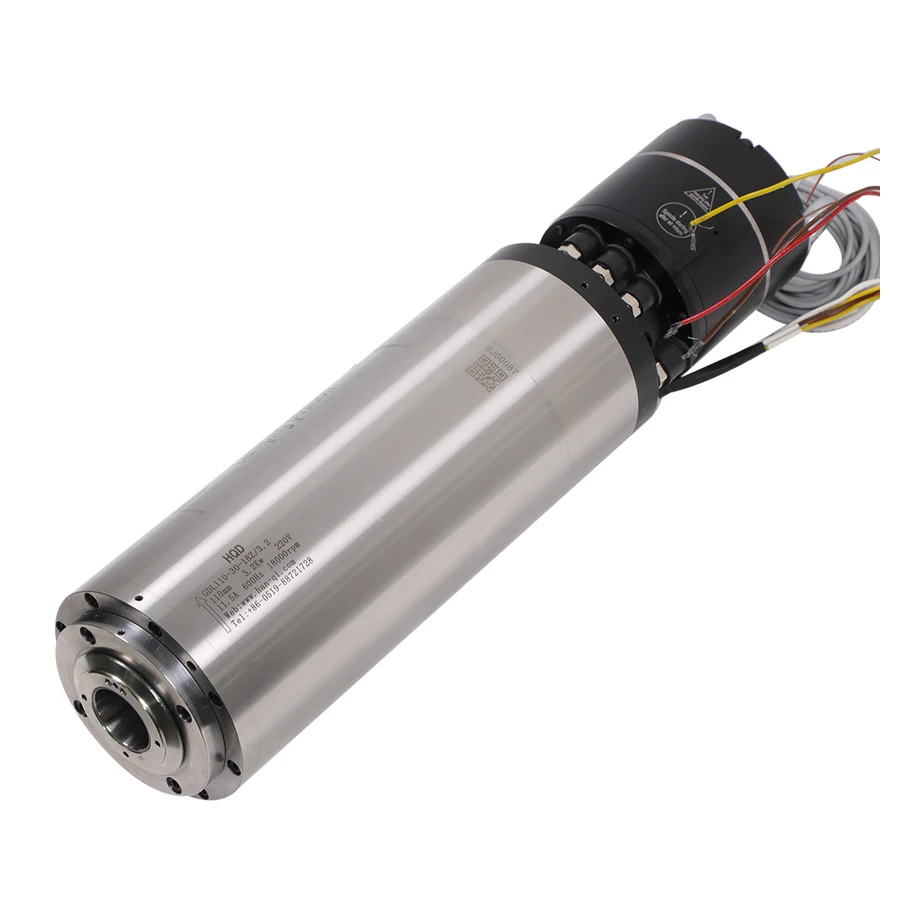
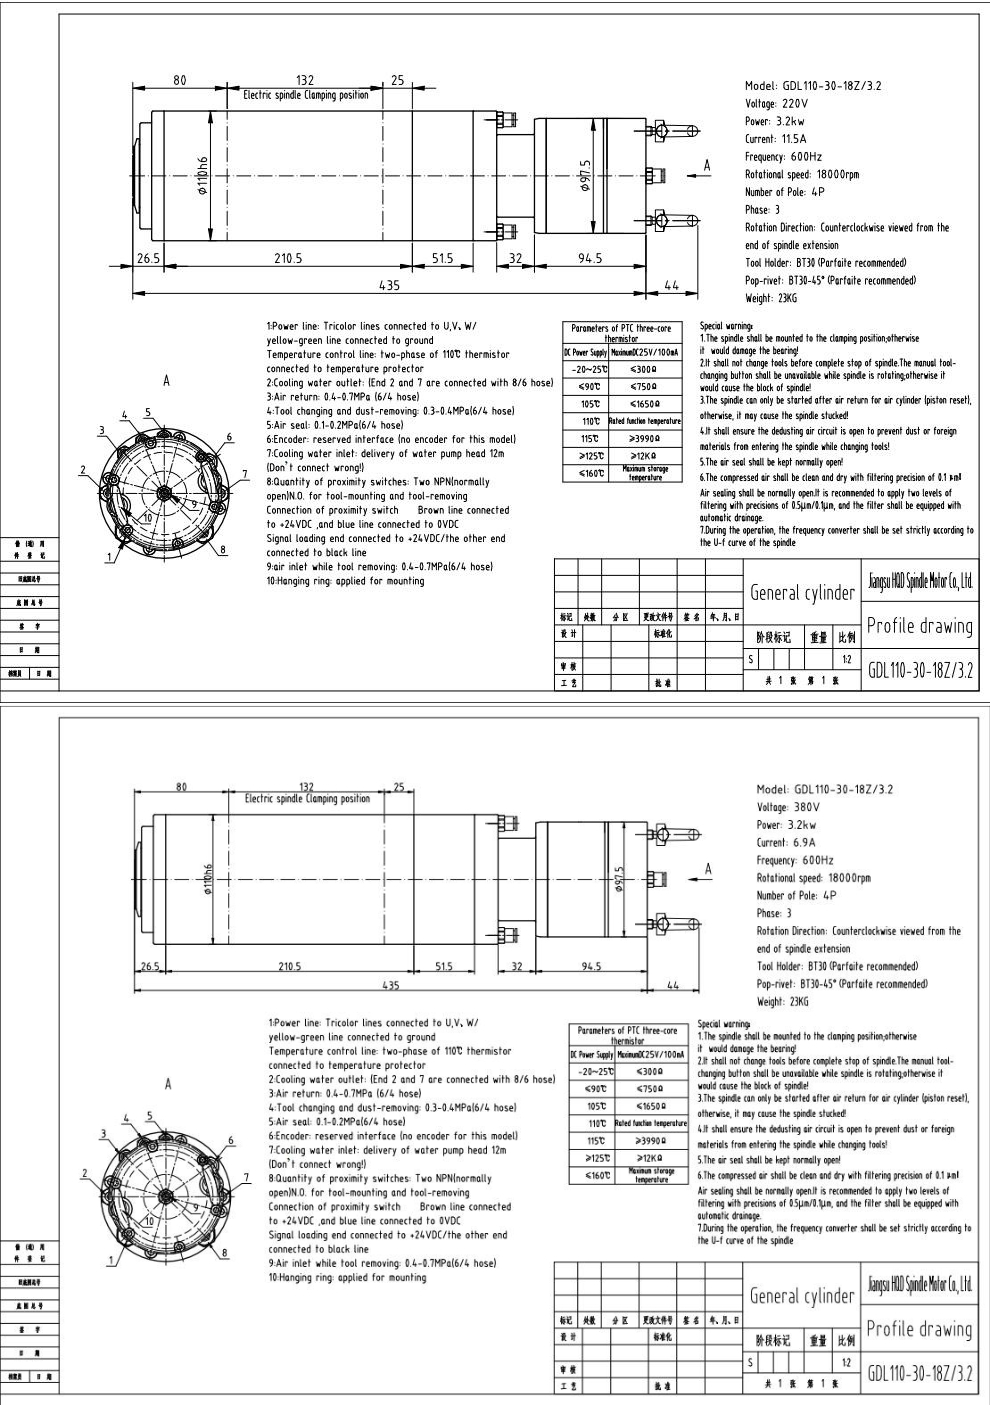
BT30 gives a specific starting point for the holder check. The complete automatic-tool-change installation still needs the correct retention arrangement, release travel, holder clearance and magazine alignment. Compare the holders and tool-change layout against the exact GDL110 assembly. A BT30 holder designation is useful evidence, but it does not confirm the rear actuator, clamp sensing or machine control sequence. Those interfaces must be reviewed before the installation is accepted.
The drawing states that no encoder is fitted. If spindle orientation or another feedback-dependent function is part of your tool-change sequence, describe that function in the inquiry. Confirm the proposed spindle and control arrangement can meet it instead of assuming that the controller can obtain feedback from an unspecified connector. The spindle's speed command and the machine's position or orientation requirement are different integration questions.
Obtain the supplied-unit pneumatic and sensor connection details before choosing release settings or wiring the control. Compare signal states with the controller and establish the interlocks needed before rotation, release and magazine movement. Confirm release pressure and the tool-change sequence from the supplied-unit instructions and the machine controller requirements. Where the existing machine uses a particular release method, include photographs and the current sequence so the technical discussion can address the actual differences.